Key takeaways
- Solder oxidises continuously at high temperature, so tin content drops and must be checked and replenished.
- Estimate the pure tin addition with T = W × (A − B) ÷ (100 − A); a 500 kg pot dropping from 63% to 61.5% tin needs about 20.3 kg.
- Mix thoroughly and re-check the composition after adding tin to avoid local concentration differences.
- High-antioxidant bars suit long high-temperature runs; high-temperature bars generate about one-seventh the dross at 450°C.
- Temperature control, dross removal, alloy segregation and regular testing are the four basics of pot maintenance.
Solder bars run at high temperature in a solder pot. Tin oxidises continuously and leaves with the dross, so the alloy composition drifts from its target. The drift changes melting point, wettability and joint appearance, and can cause cold joints, bridging and excessive dross.
Pot maintenance comes down to two actions: test the composition regularly and replenish pure tin by calculation, plus control temperature and dross. This guide gives the formula and a shop-floor procedure.
Why does tin content drop?
In wave or hot-dip soldering, the molten solder surface is continuously exposed to air, forming oxide film and dross. Tin oxidises more readily than lead, so Sn-Pb alloys lose tin over time; lead-free alloys also lose tin through oxidation, dross removal and impurity accumulation.
Other factors accelerate the shift:
- Excessive pot temperature;
- Excessive or mismatched flux;
- Mixing different alloys;
- Delayed dross removal, allowing impurities to return;
- Replenishment material that does not match the pot alloy.
How to calculate the pure tin addition
STAR.I product data gives the estimation formula:
T = W × (A − B) ÷ (100 − A)
Where:
- T: pure tin to add;
- W: solder weight in the pot;
- A: specified tin percentage (target);
- B: measured tin percentage in the pot.
Worked example
A pot contains 500 kg of solder, the target tin content is 63% and the measured content is 61.5%:
T = 500 × (63 − 61.5) ÷ (100 − 63)
  = 500 × 1.5 ÷ 37
  ≈ 20.3 kg
Add approximately 20.3 kg of pure tin.
The formula is an estimate. Confirm the addition with spectrometer results, alloy type and pot condition. Mix thoroughly and re-check after addition.
Shop-floor procedure
- Sample and test: measure the pot with a direct-reading spectrometer; record W and B. Take a representative sample, not just from the surface or a corner.
- Calculate: apply the formula and confirm the purity and grade of the pure tin.
- Add safely: add tin at a permitted pot temperature. Avoid wet tools or cold ingots that can cause splashing.
- Mix thoroughly: after the tin melts completely, stir to homogenise.
- Re-check: sample again and confirm the tin content is back in range; adjust if necessary.
- Record: keep test values, addition weight, mixing time and re-check results as trend data.
High-antioxidant vs high-temperature bars
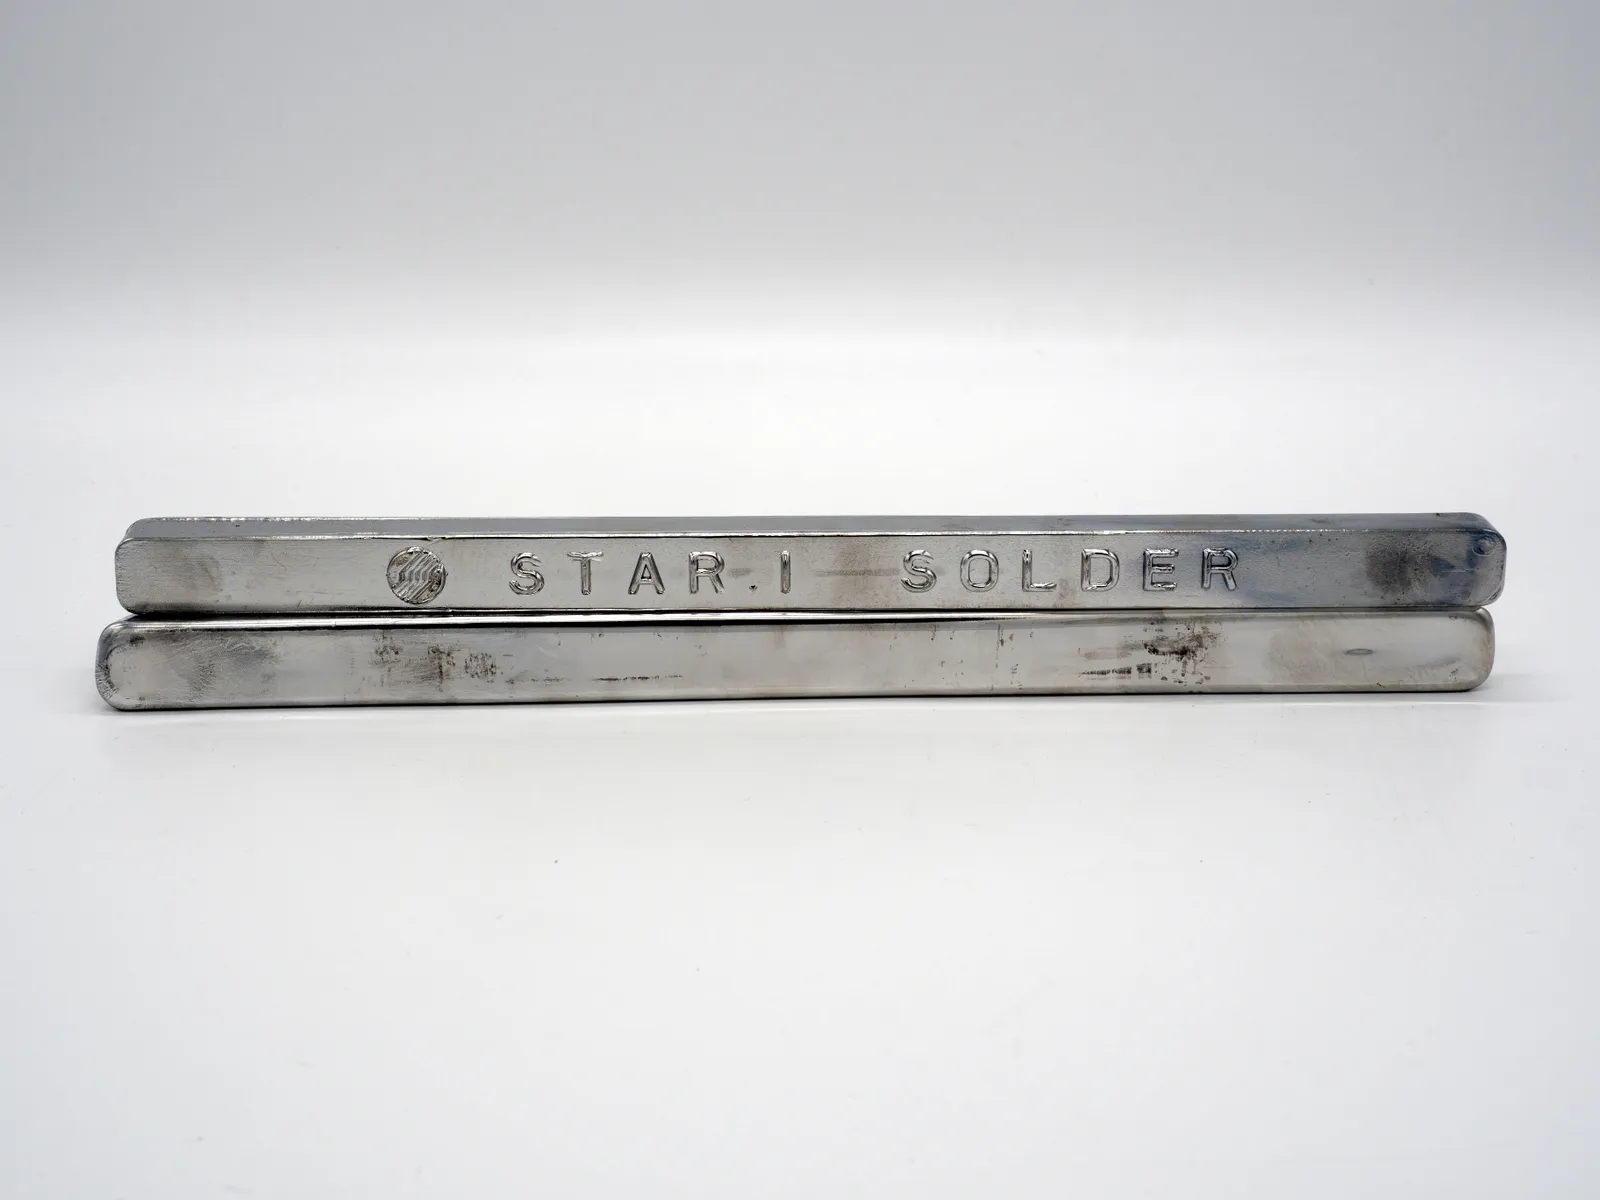
- High-antioxidant bars: below 300°C, the liquid surface stays bright and mirror-like, with short wetting time and higher spreading than ordinary solder. Suitable for pots running hot for long periods.
- High-temperature bars: at 450°C, the surface stays silver-white and mirror-like, and dross generation is about one-seventh that of ordinary bars. Suitable for high-temperature wave, hot-dip and transformer tinning.
- Lead-free bars: STAR.I recommends Sn-Cu-Ni-Ce with lead below 1000 ppm for lead-free wave soldering.
High-antioxidant bars reduce oxidation and dross; they do not eliminate dross. Temperature, flux, air contact and impurities still affect the pot.
Four basics of pot maintenance
| Action | Purpose | Guidance |
|---|---|---|
| Temperature control | Reduce oxidation and thermal damage | Set according to alloy and process; avoid prolonged overheating |
| Dross removal | Prevent impurity return and pump blockage | Remove regularly with dedicated tools; do not press dross back into the pot |
| Alloy segregation | Keep composition stable | Store and label alloys separately; clean the pot when changing |
| Regular testing | Detect composition drift early | Keep records and trend charts; adjust by measured deviation |
Common mistakes
- Watching temperature but not composition: a normal temperature does not mean a normal alloy; composition drift also causes poor joints.
- Adding a large amount at once: over-addition creates a new deviation; add in calculated steps and re-check.
- Returning dross to the pot: dross contains oxides and impurities and accelerates composition degradation.
- Mixing different alloys: even similar grades can shift melting point and wettability.
- Ignoring tools and containers: use dedicated sampling and mixing tools to avoid cross-contamination.
Conclusion
Pot maintenance is not complicated, but it must be a fixed routine: test — calculate — add — re-check — record. For pots running hot for long periods, high-antioxidant or high-temperature bars reduce dross, but temperature control, dross removal and regular testing are still essential.
For a review of your pot, share the test reports, pot capacity and process parameters with STAR.I’s technical team.
FAQ
Why does tin content drop in a solder pot?
At high temperature, tin reacts with oxygen to form tin oxide that leaves with the dross. Tin oxidises more readily than lead, so Sn-Pb alloys lose tin over time; lead-free alloys also lose tin through oxidation and dross removal. Test and replenish regularly.
What are A and B in the pure tin formula?
A is the specified tin percentage (target) and B is the measured tin percentage in the pot. T = W × (A − B) ÷ (100 − A), where W is the solder weight in the pot.
Why re-check after adding pure tin?
Local concentration differences can occur after addition. Mix thoroughly and re-test to confirm the alloy is back within specification and avoid over-addition.
Can high-antioxidant bars eliminate dross completely?
No. They reduce oxidation and dross generation, but dross still forms from temperature, flux, air contact and impurity accumulation. Regular dross removal and testing are still required.
Can different solder bar alloys be mixed?
Not recommended. Mixing changes composition and melting point, affecting wettability and joint reliability. Store alloys separately, label clearly and clean the pot when changing alloys.
References
- STAR.I TECHNOLOGY solder bar product data (pure tin formula and example)
- STAR.I TECHNOLOGY solder bar product data (high-antioxidant and high-temperature bars)
- GB 8012 Cast tin-lead solder
- JIS Z 3283 Resin-core soft solder