Key takeaways
- Choose the process first, then the alloy; reflow, wave and hand soldering have different candidates.
- SAC305 (Sn-Ag-Cu) melts at about 217–220°C and is the general-purpose reflow choice.
- Sn-Cu0.7 and Sn-Cu-Ni-Ce melt at about 227°C and are common in wave soldering; Sn-Cu-Ni-Ce is usually more stable in wetting and oxidation resistance.
- Sn-58Bi (138°C) and Sn-50In (117–125°C) suit low-temperature applications but require brittleness and reliability assessment.
- Confirm the final choice with a pilot run, wettability test and reliability validation.
Lead-free alloy selection is a balance between process window, wettability, reliability and cost. Melting points can differ by more than 100°C, and the suitable soldering method changes accordingly. This guide starts with a comparison table, then gives recommendations for reflow, wave and hand soldering.
Step 1: Define the soldering process
Do not start with “the lowest melting point” or “the cheapest alloy”. Answer three questions first:
- Which soldering method? SMT reflow, wave/hot-dip, or hand/iron soldering — each uses different product forms and alloys.
- How much heat can the components and PCB take? Component limits, board thickness and assembly density determine the usable peak temperature and dwell time.
- What reliability class is required? Consumer, industrial and automotive electronics have different thermal fatigue, drop and long-term stability requirements.
Once the process is fixed, screen the alloy table instead of working backwards.
Common lead-free alloys
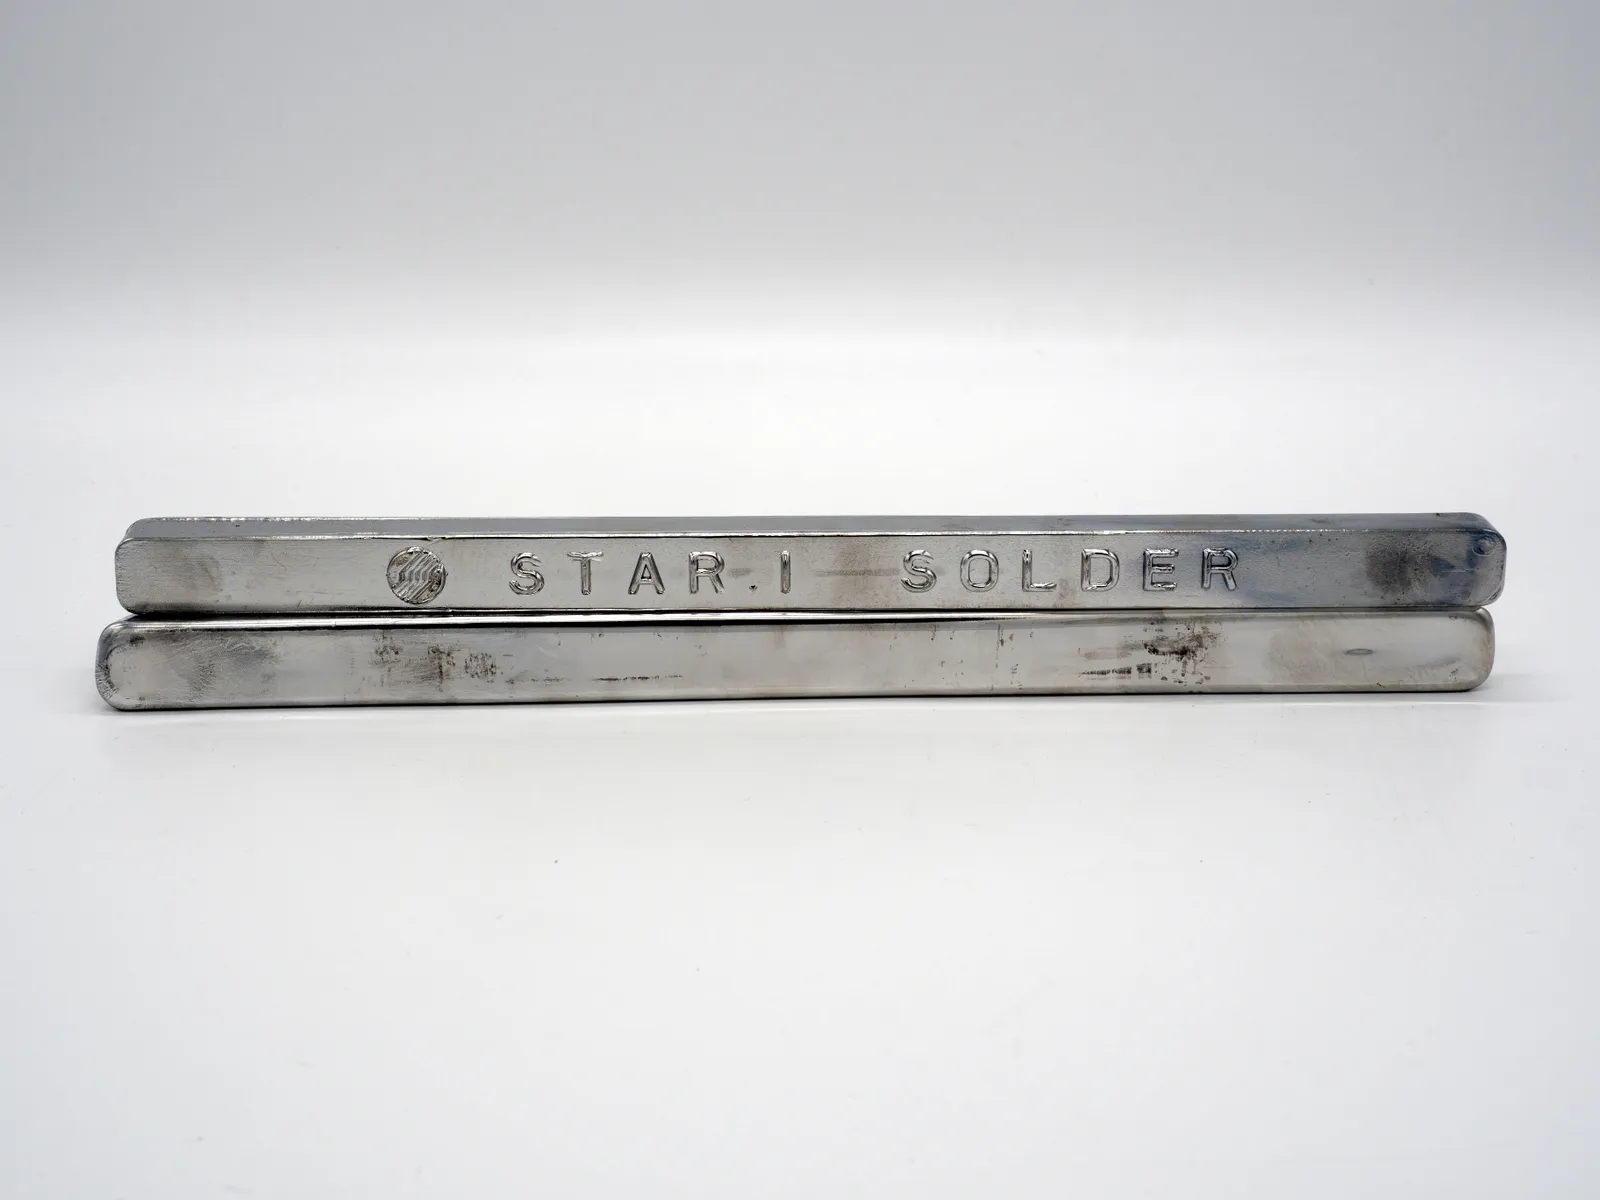
The table below lists common alloys and melting points. Data comes from STAR.I product information; always confirm with the supplier’s current TDS and batch report.
| Alloy (wt%) | Melting point (°C) | Characteristics and typical use |
|---|---|---|
| Sn-Ag-Cu (SAC305) | 217–220 | Mature process window, balanced wetting, strength and thermal fatigue; general SMT reflow |
| Sn-Cu0.7 | 227 | Lower cost, common in wave soldering; moderate wetting, needs matching flux |
| Sn-Cu0.5Ni0.1Ce0.03 | 227 | Recommended wave-soldering system; usually more stable wetting and oxidation resistance |
| Sn-Ag3.5 | 221 | Near-eutectic; good thermal fatigue resistance |
| Sn-58Bi | 138 | Low-temperature soldering for heat-sensitive parts; assess brittleness |
| Sn-50In | 117–125 | Even lower melting point for special low-temperature use; higher cost |
| Sn-Sb5 | 232–240 | High-temperature, high-strength applications; confirm component limits |
| Sn-Zn-Bi | 180–198 | Low-melting zinc-based alloy; oxidation-sensitive, demanding on flux |
Melting points are reference values near the solidus/liquidus. Actual soldering temperature also depends on pad thermal mass, oven profile and the alloy’s melting range.
Five selection dimensions
1. Melting point and process window
Melting point determines reflow peak, pot temperature and thermal damage risk. The difference between SAC305 (217–220°C) and Sn-Cu (227°C) looks small, but it can matter for heat-sensitive components, thick boards and dense assemblies.
Lead-free windows are generally narrower than Sn-Pb. Too low a peak causes poor wetting and cold joints; too high accelerates oxidation and damages components and boards. Measure the profile with a profiler instead of copying a reference curve.
2. Wettability
Wettability affects spreading and fillet formation. Sn-Pb generally wets better than lead-free alloys; within lead-free systems, SAC alloys usually wet better than Sn-Cu. If wetting is insufficient:
- Select a flux matched to the alloy and surface;
- Use nitrogen to reduce oxidation;
- Optimise preheat and reflow;
- Check pad and lead solderability.
3. Mechanical reliability and thermal fatigue
SAC alloys generally offer better strength and thermal fatigue resistance than Sn-Cu, suiting larger temperature cycles. Sn-58Bi has high strength, but high bismuth content can increase brittleness; drop and thermal shock performance need evaluation. Sn-Sb systems perform well at high temperature but require components and boards rated for the higher melting point.
4. Cost and supply
Alloy cost depends on silver, bismuth and indium prices. SAC305 contains silver and costs more than Sn-Cu0.7; Sn-50In contains indium and is usually more expensive. Compare “material cost + process yield + rework cost”, not price per kilogram alone.
5. Regulations
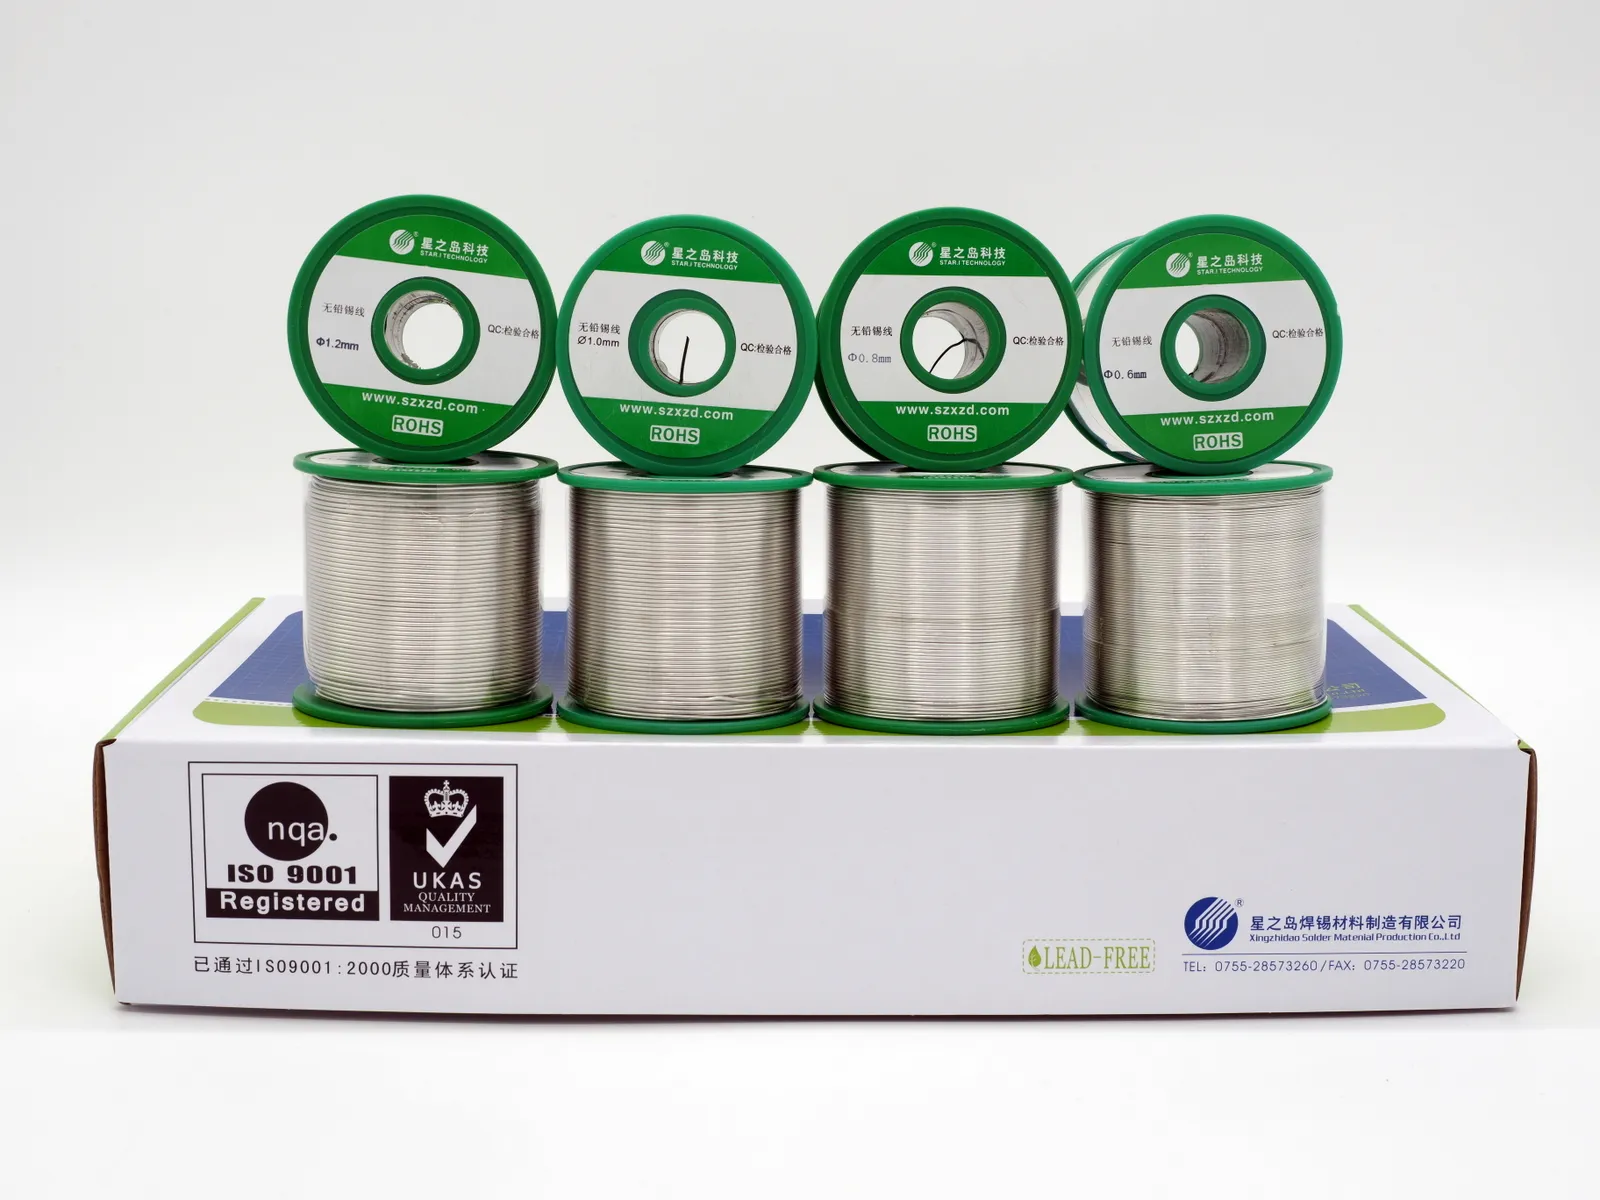
RoHS generally limits lead to below 0.1 wt% (1000 ppm) in homogeneous materials. STAR.I controls lead below 1000 ppm and cadmium below 20 ppm in its lead-free series, with SGS reports. Export products may need to meet additional market-specific regulations.
Typical recommendations
| Scenario | Recommended alloy | Reason | Watch out for |
|---|---|---|---|
| General SMT reflow | SAC305 | Mature, balanced properties | Peak around 235–245°C; measure the profile |
| Cost-sensitive wave | Sn-Cu0.7 | Low cost, 227°C | Moderate wetting; match the flux |
| Stability-first wave | Sn-Cu-Ni-Ce | Better wetting and oxidation resistance | Control pot temperature and dross |
| Low-temperature | Sn-58Bi | 138°C, less thermal damage | Assess brittleness and drop performance |
| High temperature / high thermal mass | Sn-Sb5 | High-temperature strength | Confirm component and PCB limits |
| Hand soldering / rework | SAC305 or Sn-Cu0.7 wire | Matches board alloy | Choose diameter and flux by joint |
Reflow peaks in the table are engineering references, not fixed recipes. Set the actual peak from the paste datasheet, board thickness, component limits and measured profile.
Validation checklist
Before volume production:
- Pilot run with the actual PCB, components and process parameters.
- Wettability test: spreading, fillet and cold-joint inspection.
- Joint appearance: bright, full fillets, no bridging or solder balls.
- X-ray or cross-section: void rate and intermetallic compound layer.
- Reliability: thermal cycling, thermal shock, drop or vibration, according to product class.
- Residue and insulation resistance, especially for no-clean processes.
- Batch consistency: alloy composition and impurities within specification.
Conclusion
- General reflow: SAC305 is the mature, balanced choice.
- Wave soldering: Sn-Cu0.7 for cost; Sn-Cu-Ni-Ce for stability.
- Low temperature: Sn-58Bi or Sn-50In, with brittleness and reliability assessment.
- High temperature: Sn-Sb systems, after confirming component and PCB limits.
- Every case: validate with a pilot run before volume production.
If you already know the process and product type, share the PCB finish, component temperature limits, product form and target market with STAR.I’s technical team to narrow the alloy range and arrange samples.
FAQ
Is SAC305 better than Sn-Cu0.7?
Neither is universally better. SAC305 melts at about 217–220°C with balanced wetting and thermal fatigue performance, suiting reflow. Sn-Cu0.7 melts at about 227°C and is lower cost, commonly used in wave soldering. Validate against the process window, reliability and cost.
Why is lead-free solder harder to use than Sn-Pb?
Lead-free alloys generally have higher melting points and lower wettability, with a narrower process window. They are more sensitive to flux, profile and atmosphere. Suitable alloys, flux and nitrogen can improve results.
What do Ni and Ce do in Sn-Cu-Ni-Ce?
Adding Ni and Ce to Sn-Cu generally refines the microstructure and improves wettability and oxidation resistance, stabilising joint appearance. Confirm the effect with the specific alloy, pot conditions and process validation.
Is low-temperature solder always more reliable?
No. Low-temperature alloys such as Sn-58Bi reduce thermal damage, but higher bismuth content can increase brittleness risk. Drop and thermal-shock performance must be evaluated.
References
- STAR.I TECHNOLOGY lead-free solder product data (alloy and melting point table)
- GB 3131 Tin-lead solder and GB 8012 Cast tin-lead solder
- JIS Z 3283 Resin-core soft solder
- EU RoHS Directive 2011/65/EU and amendments
- US QQ-S-571E industrial specification